lvobo blog
Home

Laboratory Sieve Shaker

Laboratory Sieve Shaker

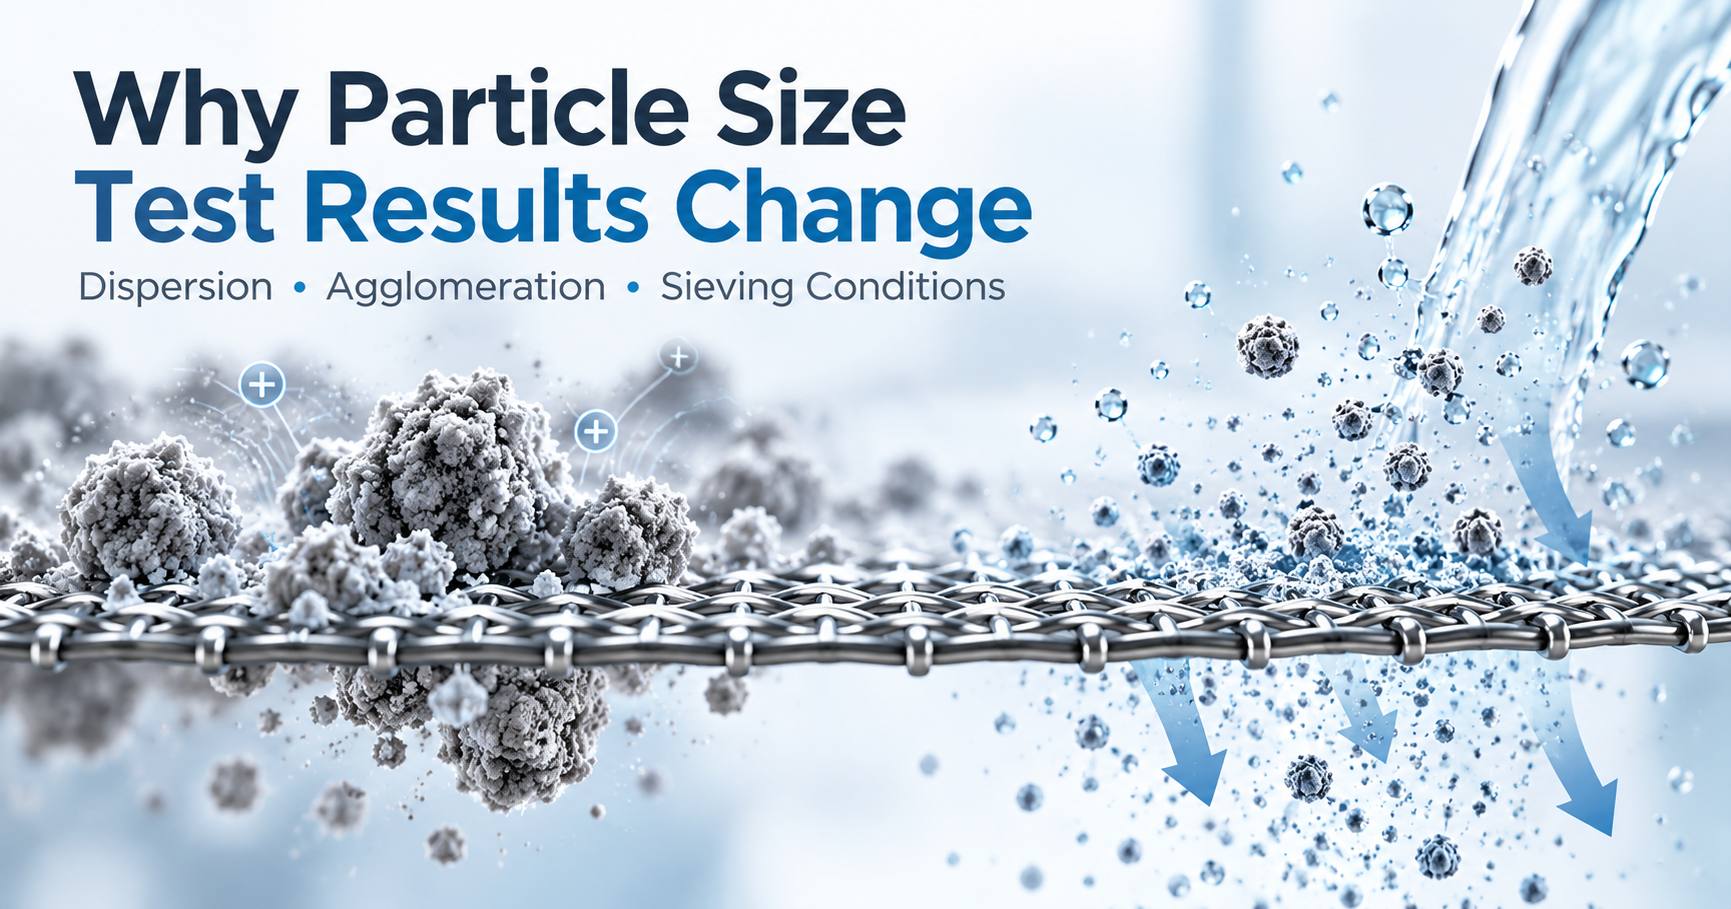
  • Why Particle Size Test Results Change: Dispersion, Agglomeration and Sieving Conditions
    Why Particle Size Test Results Change: Dispersion, Agglomeration and Sieving Conditions
    Oct 26, 2026
    Particle size is often treated as a fixed property of a powder. In practice, however, the reported result also depends on the physical state of the sample and the method used to measure it. A powder tested in an agglomerated dry state may behave differently after liquid dispersion. Fine particles affected by static electricity may remain on a test sieve even when their dimensions would otherwise allow them to pass. Changes in sample preparation, sieving time, dispersion conditions, or measurement principle can also affect the reported particle size distribution. This means that when two laboratories test the same material and obtain different results, neither laboratory has necessarily made an error. For QC and procurement engineers, the more useful question is not simply: “What is the particle size?” It is: “Under what sample condition and test method was that particle size measured?” Why Do Particle Size Test Results Change? Particle size results can change because the powder state and test conditions change. Agglomeration, dispersion, static electricity, wet or dry testing, sample preparation, test duration, and measurement principle can all affect the reported particle size distribution. Results should only be compared when the test method and sample conditions are controlled. When Agglomeration Makes Fine Powder Look Coarser Fine powders do not always behave as independent particles. Moisture, electrostatic attraction, surface forces, and handling conditions can cause smaller particles to associate with one another. When this happens, a test may respond to the agglomerate rather than to the individual particles inside it. In mechanical sieving, an agglomerate may remain above the sieve opening even though the individual particles would be small enough to pass. The retained fraction may therefore contain both genuinely oversized particles and clusters of smaller particles that have not been sufficiently dispersed. For supplier qualification, batch comparison, or incoming inspection, sample preparation and dispersion conditions should be controlled before numerical results are compared. When Dispersion Changes the Measured Distribution Dispersion can also change what the measurement system sees. A recent Malvern Panalytical application study used time-resolved laser diffraction to monitor spray-dried alumina granules during ultrasonic dispersion. As dispersion progressed, a coarser particle population decreased while a finer population became more pronounced. The important point is not the individual particle-size values. It is that the measured distribution changed as the physical state of the sample changed. Ultrasonic energy, liquid media, mixing conditions, and dispersion time may separate agglomerates or otherwise alter the particle population presented to the measurement system. This creates a practical laboratory question: At what point does dispersion reveal the particle state relevant to the application, and at what point does additional energy begin to alter that state? There is no universal answer. Different materials can respond differently to the same preparation procedure. For this reason, particle size methods should specify not only the instrument, but also the sample preparation and dispersion conditions. When Static Electricity Distorts Dry Sieving Dry sieve analysis introduces another important source of variation: electrostatic charge. Fine particles may adhere to the sieve mesh, sieve frame, container surfaces, or other particles. This can make an electrostatic problem look like a particle-size problem. If fine powder remains above the sieve, the immediate conclusion may be that those particles are larger than the sieve opening. But some particles may actually be small enough to pass and remain on the mesh because of static attraction or loose agglomeration. Increasing vibration does not necessarily eliminate the underlying electrostatic interaction. For laboratory sieve analysis, visible adhesion to the mesh or frame should therefore be treated as a warning that the retained fraction may contain more than genuinely oversized particles. This is especially relevant for fine polymer powders, pharmaceutical materials, chemical powders, and other materials prone to electrostatic charging. Why Wet Sieving Can Produce a Different Result Wet sieving can reduce problems associated with agglomeration, static electricity, or persistent mesh blockage. But wet sieving is not simply dry sieving with liquid added. The liquid becomes part of the test method. A suitable medium may improve dispersion, reduce static effects, and help fine particles pass through the sieve. At the same time, it may also alter the sample. Depending on the material and liquid, particles may dissolve, swell, soften, react chemically, or experience changes in surface behavior. A controlled wet-sieving method should therefore define the liquid medium, sample preparation, dispersing agents, rinsing procedure, drainage conditions, test duration, and endpoint criteria. The objective is not simply to make more material pass through the sieve. The laboratory should first determine whether high residue in dry sieving represents genuinely oversized particles or poor particle dispersion. For applications affected by static electricity, agglomeration, or wet-sieving conditions, our laboratory sieve shaker selection guide explains how these factors should be considered during equipment selection. Why Sieving Time and Endpoint Criteria Matter Sieving time can also change the reported result. Consider two laboratories testing the same powder with the same nominal sieve aperture. One runs the sieve shaker for five minutes. The other runs it for fifteen minutes. If material continues to pass through the sieve after the first five minutes, the two laboratories are not performing equivalent tests. Longer sieving may give particles more opportunities to reach an opening, change orientation, or separate from weak agglomerates. For this reason, instructions such as: “Sieve until it looks finished.” are unsuitable for comparative QC. When sieve analysis is used for batch release, supplier acceptance, or interlaboratory comparison, test duration or endpoint criteria should be defined in the SOP. The objective is reproducibility, not simply reducing the amount of material left above the sieve. Why Different Particle Size Methods Do Not Always Agree If two particle size reports disagree, one of the first questions should be whether the laboratories used the same measurement principle. A result expressed in micrometers does not necessarily represent the same physical quantity across different methods. Mechanical sieving determines whether a particle can pass through an opening of defined geometry under specified mechanical conditions. Laser diffraction evaluates light-scattering behavior and calculates an equivalent particle size distribution using an optical model. Dynamic image analysis evaluates projected particle images and can provide information related to both size and shape. These differences become especially important for irregular particles. An elongated particle may remain above a sieve when lying flat but pass through the same opening when it approaches at a different angle. Laser diffraction may report an equivalent diameter, while image analysis may describe length and width separately. The key point is: The same unit, μm, does not mean that different methods are measuring exactly the same physical quantity. This is why results generated by different techniques should not be compared without considering the measurement principle. Before Comparing Two Particle Size Reports, Check These 9 Conditions Before recalibrating an instrument, rejecting a batch, or questioning a supplier’s data, first determine whether the laboratories performed comparable tests. 1. Sample SourceWere the samples taken from the same batch using comparable sampling procedures? 2. Sample ConditionWere moisture level, storage conditions, and handling history comparable? 3. Sample PreparationWere drying, mixing, dividing, or other preparation procedures controlled? 4. Agglomeration and DispersionWas the material tested in a comparable and controlled physical state? 5. Measurement MethodDid both laboratories use the same analytical principle? 6. Wet or Dry ConditionsWas the powder tested under comparable environmental and dispersion conditions? 7. Sample QuantityWas a comparable amount of material introduced into each test? 8. Test DurationWere the same sieving or dispersion times used? 9. Endpoint CriteriaDid both laboratories use the same rule to determine when the test was complete? If these conditions differ, the reported particle size values may not be directly comparable even when both laboratories are operating their equipment correctly. How to Select Equipment Without Changing the Test Method The same logic should guide laboratory equipment procurement. A laboratory sieve shaker should not be selected first and then used to define the test method afterward. A more defensible sequence is: Understand powder behavior → Define the QC objective → Select the test method → Establish test conditions → Select equipment capable of repeating that method For free-flowing materials, conventional dry sieving may be appropriate. For powders affected by static electricity or agglomeration, sample preparation may need to be reconsidered, or wet sieving may need to be evaluated. For irregular particles, the mechanical motion of the sieve shaker can become part of the method. For very fine powders or applications requiring detailed particle size distributions, another analytical technique may be more suitable than mechanical sieving alone. Particle size data become useful when the conditions behind the numbers are understood. For procurement, R&D, and QC teams, reliable comparison requires more than matching the unit “μm” on two reports. It requires comparing the sample condition, test method, and operating procedure behind those numbers. When these conditions are controlled, particle size data become far more useful for batch comparison, supplier qualification, incoming quality control, process development, and material acceptance decisions.
    Read More
  • What Is a Laboratory Sieve Shaker? Working Principle, Applications, and Selection Guide
    Oct 05, 2026
    In research, quality control, and production testing involving powders, granules, and raw materials, particle size distribution can directly affect flowability, dissolution rate, mixing uniformity, reaction efficiency, and final product quality. For laboratories in industries such as chemicals, pharmaceuticals, food, advanced materials, and scientific research, achieving fast, stable, and repeatable particle separation is a fundamental but important task. A laboratory sieve shaker is designed for exactly this purpose. By using mechanical vibration, electromagnetic vibration, or multidirectional motion, a sieve shaker moves a sample through a stack of test sieves with different mesh sizes. This allows particles to be classified according to size and helps laboratories determine the percentage of material within different particle-size ranges. What Is a Laboratory Sieve Shaker? A laboratory sieve shaker is an instrument used for particle size analysis, grading, and sieve residue testing of powders and granular materials. In a typical test, several standard test sieves with different aperture sizes are stacked from coarse to fine. The sample is placed on the top sieve. Once the machine starts, continuous vibration causes the material to move, spread, and pass through the sieve openings. Larger particles remain on the upper sieves, while smaller particles gradually pass through to the lower layers. After the sieving process is completed, the material retained on each sieve can be weighed to calculate the percentage of particles within each size range. Laboratory sieve shakers are commonly used for: Particle size distribution analysis Raw material particle size testing Product quality control Sieve residue analysis Impurity ratio testing New material development Formulation and process optimization Compared with manual sieving, a laboratory sieve shaker can improve testing efficiency while reducing operator-dependent variation. How Does a Laboratory Sieve Shaker Work? The purpose of a sieve shaker is not simply to make the sieve vibrate. Its main function is to create an effective particle movement pattern on the sieve surface so that particles can separate efficiently according to size. During the sieving process, the material usually goes through three basic stages. 1. Sample Dispersion Vibration helps break up the material bed and spread particles across the sieve surface. This allows more particles to come into contact with the sieve openings. 2. Passage Through the Sieve Openings When a particle is smaller than the sieve aperture and approaches the opening at a suitable orientation, it can pass through to the next sieve. 3. Particle Size Classification As the process continues, particles of different sizes are gradually retained on different sieve levels, producing a classified particle-size distribution. Different laboratory sieve shakers use different vibration mechanisms. Some machines use vibration motors to generate mechanical motion, while electromagnetic sieve shakers use an electromagnetic excitation system to create high-frequency reciprocating vibration. Vibration intensity, sieving time, and particle movement pattern can all influence sieving efficiency and test repeatability. Why Is Repeatability Important in Laboratory Sieving? For laboratory testing, simply separating the material is usually not enough. A more important question is: Can the same sample produce similar results when tested under the same conditions? If vibration intensity, sieving time, or operating procedures vary from test to test, the results may also vary significantly. This is why modern laboratory sieve shakers increasingly use programmable and adjustable operating parameters. For example, LVOBO laboratory sieving equipment allows users to adjust operating parameters for different materials and store commonly used sieving programs. When the same material needs to be tested again, operators can quickly recall previously established settings. This reduces repeated parameter adjustment and helps laboratories create more standardized testing procedures. Such functionality is particularly useful for R&D laboratories, quality-control laboratories, and companies that perform regular batch testing. What Materials Can Be Tested with a Laboratory Sieve Shaker? Laboratory sieving equipment can be used for a wide range of powders and granular materials. Chemical Materials Examples include resin powders, pigments, coating powders, chemical raw materials, and functional powders. Particle size can affect dispersion, reaction performance, processing behavior, and product consistency. Pharmaceutical and Biopharmaceutical Materials Drug powders, excipients, and certain granular formulations often require particle size control during development and production. A controlled particle size distribution can contribute to more consistent product performance. Food Materials Flour, starch, seasonings, food additives, sugar powder, and other food powders can be tested for particle size or impurities using laboratory sieving equipment. Advanced Materials Applications include metal powders, ceramic powders, battery materials, 3D-printing powders, and other functional materials. For many of these materials, particle size distribution is closely related to downstream processing performance. Universities and Research Laboratories Research institutes and universities can use laboratory sieve shakers for material development, particle analysis, formulation studies, and process validation. Minerals, grains, plastic granules, and many other particulate materials can also be tested depending on the specific application. How to Choose the Right Laboratory Sieve Shaker When selecting a laboratory sieve shaker, it is not enough to compare only machine power or price. The selection should be based on the sample characteristics and testing requirements. 1. Particle Size Range First, determine the particle size range that needs to be analyzed. Different test sieves have different aperture sizes, so the sieve specifications should match the target particle-size range. For a wide distribution, multiple sieves with different mesh sizes can be stacked together. 2. Sieve Diameter Standard laboratory test sieves are available in different diameters. Before selecting a machine, confirm that it is compatible with the test sieve sizes already used in your laboratory or planned for future use. 3. Sample Quantity The amount of material used in one test may range from only a few grams to several hundred grams or more. Excessive loading can reduce sieving efficiency, so the machine and sieve diameter should be selected according to the typical sample quantity. 4. Vibration Method Different vibration systems provide different operating characteristics. Traditional vibration-motor systems are widely used and suitable for many routine laboratory sieving applications. Electromagnetic sieve shakers use high-frequency electromagnetic excitation and can be suitable for applications requiring precise vibration control and good repeatability. 5. Adjustable Parameters Different powders may require different sieving conditions. A machine that allows users to adjust vibration intensity, operating time, and vibration mode provides greater flexibility for optimizing the process for different materials. 6. Program Storage If a laboratory regularly tests several standard materials, program memory can significantly improve efficiency. Operators can save different sieving parameters for different materials and recall them during future tests. This can also support the development of standardized operating procedures, or SOPs. Why Are Multiple Test Sieves Important? Laboratory particle size analysis is usually not just about determining whether particles are “large” or “small.” The goal is often to understand the full particle size distribution. For example, a sieve stack may be arranged as follows: 500 μm↓250 μm↓125 μm↓63 μm↓Receiving Pan After sieving, particles within different size ranges remain on different sieves. By weighing the material retained on each sieve, the percentage of each fraction can be calculated. A common calculation is: Sieve Retention (%) = Weight Retained on the Sieve ÷ Total Sample Weight × 100% This provides a clearer picture of the particle-size composition of the sample. For product development and quality control, such data are generally more useful than evaluating powder appearance alone. How Can You Improve the Reliability of Laboratory Sieving Results? To obtain more consistent results, important testing conditions should remain as stable as possible. Recommended practices include: Use test sieves of the same specification and condition Maintain a consistent sample weight Use a fixed sieving time Keep vibration settings consistent Prevent excessive sieve blockage Clean sieves regularly Establish standard testing programs for recurring materials Some powders may also be prone to agglomeration, static electricity, or irregular particle behavior. For these materials, additional optimization of the sieving parameters may be required. There is no single vibration setting that works perfectly for every powder. For this reason, establishing a dedicated sieving program for each material through repeated testing can help improve data consistency. LVOBO Laboratory Sieving Solutions LVOBO focuses on the development and manufacture of laboratory sieving equipment and related laboratory instruments. To meet different particle-testing requirements, we provide multiple laboratory sieving solutions, including vibratory sieve shakers and electromagnetic sieve shakers. LVOBO's latest laboratory vibratory sieve shakers feature touchscreen control and adjustable operating parameters. Depending on the material, users can adjust forward motion, reverse motion, vertical vibration, operating time, and cycle settings. The system also supports storing multiple commonly used sieving programs. When the same or similar material is tested again, operators can quickly recall previous settings, reducing repetitive setup work. For applications requiring high-frequency vibration, the LVOBO BO-300ESS Electromagnetic Sieve Shaker uses an electromagnetic excitation system to generate high-frequency reciprocating motion. Its vibration amplitude, vibration interval, and sieving time can be adjusted according to different testing requirements. Different sieving technologies are suitable for different laboratory conditions. For this reason, we recommend selecting a sieve shaker based on the sample type, target particle size, sieve specifications, sample quantity, and testing workflow rather than evaluating the machine only by power or vibration amplitude. Conclusion Particle size is one of the most important basic parameters for powders and granular materials. A suitable laboratory sieve shaker does more than simply separate particles. More importantly, it helps laboratories establish a stable and repeatable particle-size testing process. Before choosing a sieve shaker, consider the following questions: What material do you need to sieve? What particle-size range do you need to analyze? What diameter of standard test sieve will you use? How much material will you test each time? Do you need to save and recall sieving programs? Selecting equipment based on these factors is usually more effective than comparing only power, amplitude, or price. If you are looking for laboratory sieving equipment for powders, granules, or particle size analysis, contact LVOBO. Our team can help you select a suitable laboratory sieving solution based on your sample type, sieve specifications, and testing requirements.
    Read More
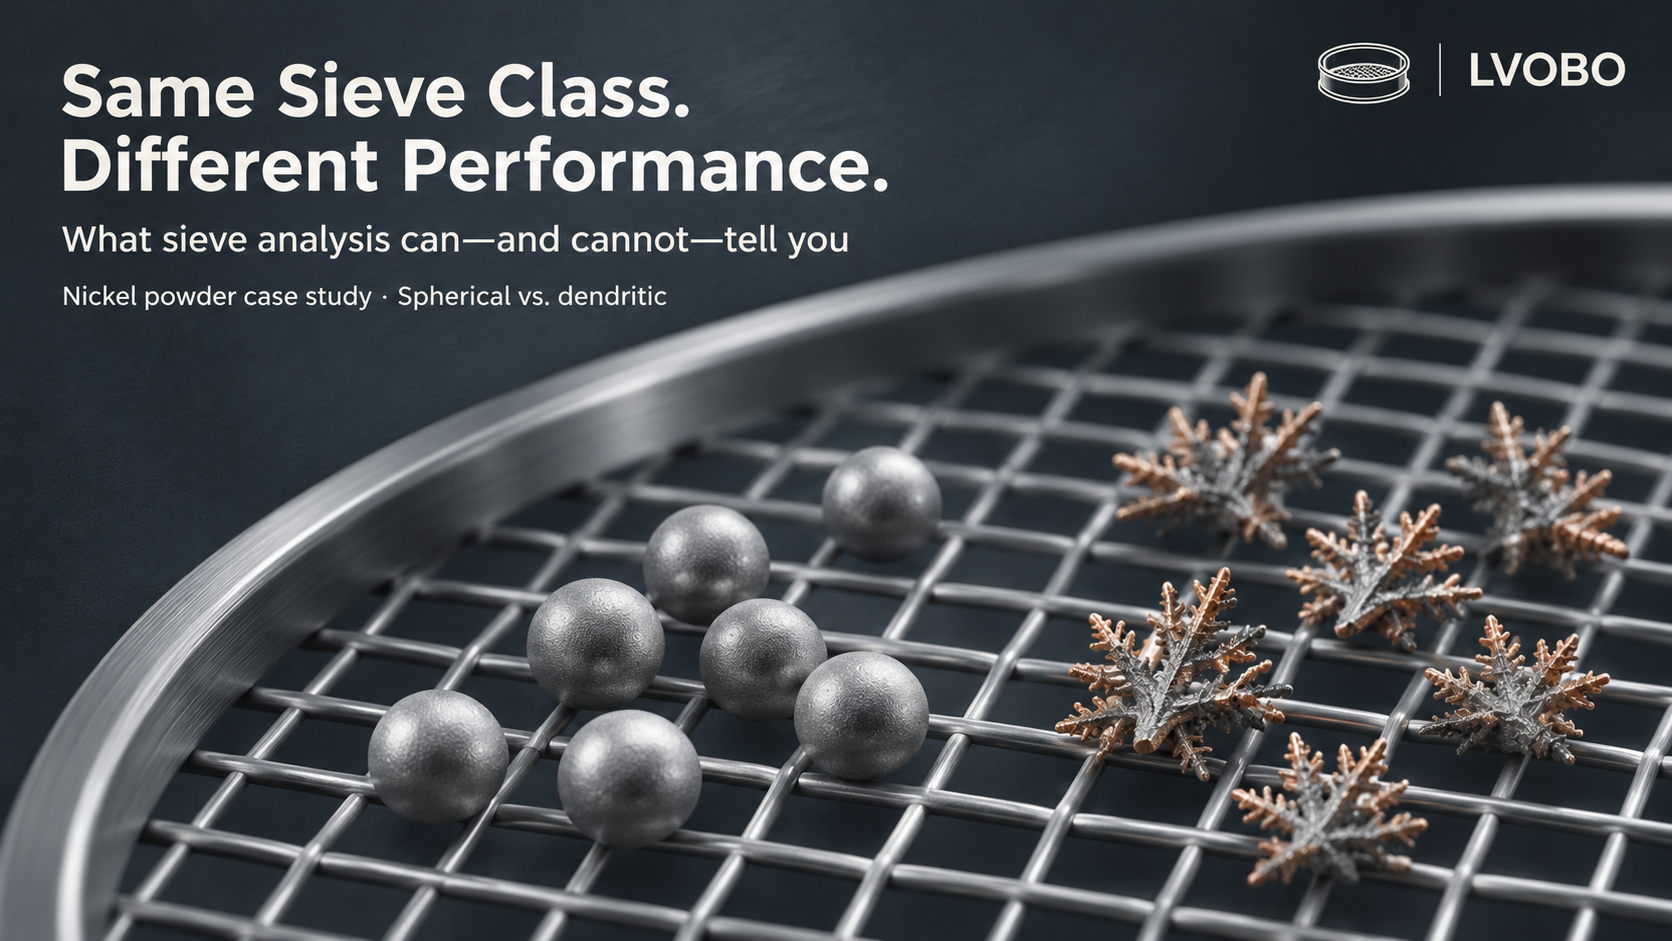
  • Particle Size vs. Particle Shape: Why Sieve Analysis Is Only the Starting Point
    Particle Size vs. Particle Shape: Why Sieve Analysis Is Only the Starting Point
    Nov 01, 2026
    In powder procurement and quality control, particle size is often the first metric written into a specification. Once the powder passes through the sieve, falls into the specified size fraction, and the report shows "Pass," the process for many stops there. But here is the question: Does particle size compliance truly equal powder performance compliance? A recent 2026 study on commercial nickel powders by a South Korean research team, published in the Journal of Powder Materials, offers a blunt reminder: Not necessarily. The researchers compared spherical and dendritic nickel powders, further dividing each morphology into two sieve classes: 25–32 μm and 32–45 μm. They found that within the tested sample groups, changing the sieve classification had a relatively limited impact on resistivity, while the difference in electrical behavior between the spherical and dendritic groups was striking. Under matched pressure conditions, the reported resistivity values differed by a factor of approximately 16 to 70, depending on the pressure conditions and sample pairs. This is not to say sieving is unimportant. Sieving is, of course, crucial—it is a fundamental tool for particle size control. But it answers a very narrow question: Can this powder pass through this sieve aperture, and which size fraction does it fall into? It does not answer whether the particles are spherical or dendritic, whether the surface is oxidized, whether the supplier's process is consistent, and it certainly does not answer how this powder will actually perform in pressure-conductive rubber. The Core Pain Point of Sieve Reports: It Looks Too Much Like a "Complete Answer" Sieving analysis is highly practical in the lab. It can tell you: The mass retained on each sieve aperture; The proportion of material within the specified size fraction; The presence of oversized particles; Whether there are variations in particle size distribution between batches; Whether the powder meets sieve-based acceptance criteria. This information is valuable. The problem is that many procurement and quality processes equate "meeting sieve acceptance criteria" directly with "stable powder quality." This is a dangerous leap. Powders within the same sieve class can be completely different in the following aspects: Particle morphology: spherical, dendritic, irregular, or flake-like; Surface structure: roughness, oxide layer, surface treatment; Inter-particle contact mode: point contact, surface contact, branched interlocking; Specific surface area and flowability; Resistivity, filling behavior, or processing performance in actual applications. A sieve report won't tell you these things. It cannot independently determine whether particles are spherical or dendritic, cannot quantify surface roughness, cannot identify surface oxidation, and cannot measure resistivity. Using sieve analysis for these tasks is like using a bathroom scale to judge a person's health—weight matters, but it’s not the whole story. What's Really Striking About This South Korean Nickel Powder Study: Same Sieve Class, Performance Can Differ by an Order of Magnitude The study focused on nickel powders used in pressure-conductive rubber semiconductor test sockets. The researchers compared four commercial nickel powder samples with two morphologies: spherical and dendritic; each morphology was further divided into two sieve classes: 25–32 μm and 32–45 μm. They evaluated particle size distribution, surface area, true density, particle morphology, and resistivity under different compression pressures. The results are clear: within the tested sample groups, sieve class variation had a relatively limited impact on resistivity, while the difference between the spherical and dendritic groups was very large. Dendritic powders exhibited lower resistivity or formed effective conductive contacts earlier at lower compression pressures; under matched pressure conditions, the resistivity of the two groups differed by a factor of approximately 16 to 70. A crucial caveat must be stated: the spherical and dendritic powders came from different suppliers. Therefore, this difference is a combined effect of morphology and supplier factors, and cannot prove that particle morphology alone caused all the differences. The supplier's manufacturing process, surface state, impurity control, and oxidation degree may all play a role. But it is precisely this caveat that makes the conclusion even more impactful for procurement and quality control: the sieve report you receive doesn't even cover the variables that truly affect performance—"morphology + supplier + surface state." Particle size compliance might just be "looking compliant." Even More Provocative: Sieve and Laser Diffraction Results Might Naturally Be Inconsistent The study includes an interesting detail. The researchers first separated the nickel powder into a 25–32 μm sieve class, then measured the particle size distribution using laser diffraction. The reported laser diffraction D50 values for the spherical and dendritic samples were approximately 34.9 μm and 35.5 μm, respectively. At first glance, this seems contradictory to the sieve class. But it’s not that sieving must be wrong; rather, the two methods measure different things. Mechanical sieving looks at whether a particle can pass through a sieve aperture under specified conditions; for non-spherical particles, passage depends on the effective cross-section and orientation. Laser diffraction calculates an equivalent spherical diameter; an elongated or branched particle might pass through a sieve aperture in a favorable orientation but yield a larger equivalent spherical diameter in laser diffraction. D50 is the median equivalent spherical diameter, not the sieve upper limit. Therefore, inconsistency between sieve and laser diffraction results does not automatically mean a testing error. It just reminds you that different measurement principles answer different questions. For powder engineers, when comparing supplier reports, if the particle size analysis methods differ, directly comparing the numbers is risky. What Sieve Analysis Should and Should Not Do Sieve analysis should continue to be done, and done well. It is a fundamental tool for laboratory particle size analysis and quality control. But it should not be treated as a complete evaluation of powder performance. Sieve analysis confirms particle size distribution and sieve residue; it cannot replace SEM for morphology, image analysis for shape quantification, surface analysis for oxidation, or application testing for resistivity, flowability, or filling behavior. A more reasonable powder evaluation workflow should be divided into three layers: Particle Size Classification: Use test sieves and controlled screening procedures to confirm size fractions, retained mass, and oversized particles. Particle Morphology: Use microscopy or image analysis to check if particles are spherical, dendritic, or irregular, and whether the surface structure is consistent. Application-Specific Performance: Directly measure metrics relevant to the application scenario, such as resistivity, flowability, surface area, and chemical composition. Not every powder requires all three layers. But if your application is sensitive to morphology, contact structure, or electrical conductivity, looking only at a sieve report is far from enough. The Role of Laboratory Sieve Shakers: Do Particle Size Control Solidly, But Don't Make It Take the Blame It Shouldn't For laboratories handling metal powders, chemical powders, pharmaceutical materials, and advanced materials, laboratory sieve shakers remain core equipment for particle size control. Compared to manual sieving, programmable laboratory sieve shakers standardize mechanical motion, operating time, and testing procedures, making sieve results between batches more comparable. LVOBO laboratory sieve shakers, including the BO-200SY and BO-300SY models, are designed for laboratory particle size analysis, powder classification, and sieve residue testing. Selected configurations offer programmable screening functions such as forward/reverse motion, vertical vibration control, operating time and cycle settings, and storage for multiple test programs; specific functions depend on the configuration. But the equipment's role must be clearly stated: a sieve shaker determines how material passes through selected apertures; it does not replace SEM, image analysis, surface analysis, or resistivity testing. It is the starting point of particle size control, not the endpoint of powder quality. Using the sieve shaker correctly means controlling the particle size variable; treating the sieve report as a complete quality conclusion leaves the risk to downstream processes. Conclusion: Particle Size Compliance is Just the Starting Point, Not the Endpoint The core takeaway from this South Korean nickel powder study for procurement engineers, R&D teams, and quality control labs is: powders within the same sieve class can still exhibit significantly different behaviors in specific applications. And because morphology and supplier factors were confounded in the study, this result serves more as a warning: do not treat a sieve class as a complete quality description, and do not assume a sieve report covers morphology, surface state, and supplier consistency. So, to put it boldly: Sieve analysis is a must, but judging powder quality solely by sieve analysis is like using one ruler to measure an entire material system. Use sieving to control particle size, use microscopy and image analysis to examine morphology, and use application testing to evaluate actual performance. Reliable powder quality control is not about buying more instruments; it's about understanding exactly what questions each method can and cannot answer. Particle size compliance is just the starting point. True powder quality lies beyond the sieve apertures.
    Read More

leave a message

leave a message
If you are interested in our products and want to know more details,please leave a message here,we will reply you as soon as we can.
Submit

Our hours

Monday - Saturday: 8:00 AM - 6:00 PM

Contact Us:lvobo2026@gmail.com

Home

Products

whatsApp

contact